
Palatal XF 9012 is an AOC low viscosity, highly reactive unsaturated polyester resin designed for pultrusion formulations with high aluminium hydroxide loading. Its halogen-free resin system provides a processing base for composite parts requiring fire, smoke and toxicity performance. The supplied PDS explains that the resin itself is not flame retardant. The fire performance described applies to suitable resin and aluminium hydroxide combinations.
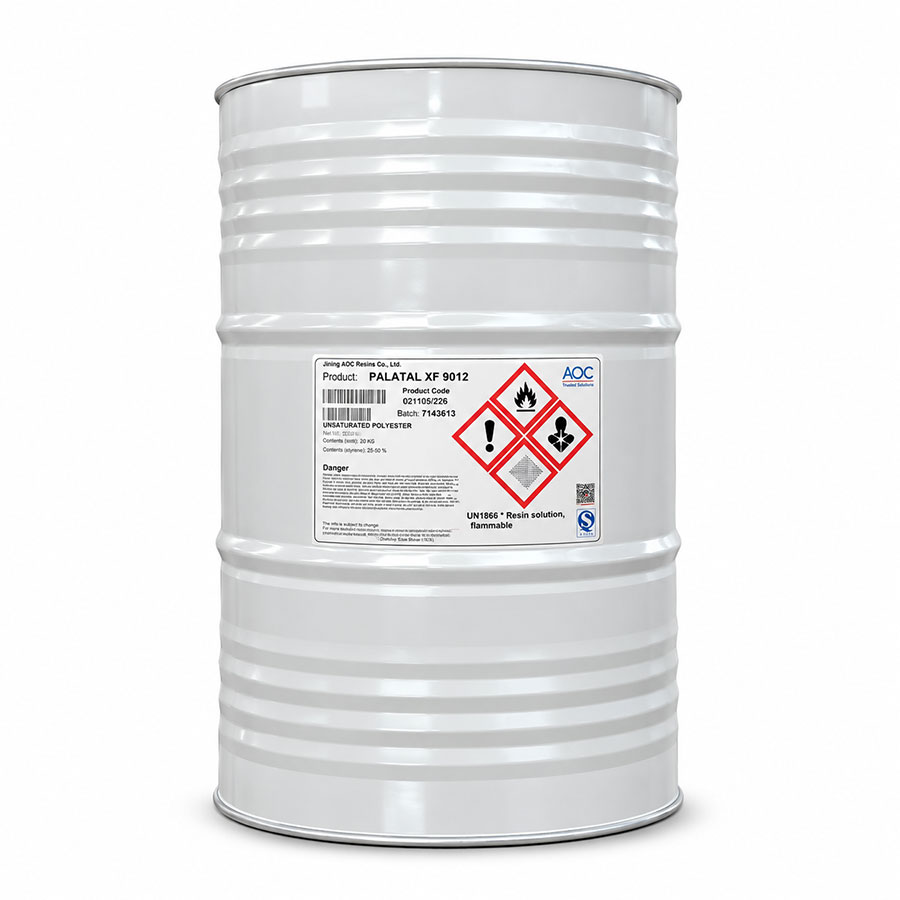
Palatal XF 9012 applications and formulation
This grade is intended for pultruded products of different sizes. Its low viscosity supports high filler incorporation, while high reactivity helps maintain processing speed in heavily filled formulations. The manufacturer also lists hand lay-up and cast grating as processing options. Where aluminium hydroxide content is high, reinforcement levels must be adjusted. Establish the balance between filler, glass reinforcement, wetting and mechanical performance for the intended profile before routine production.
Liquid resin specifications
| Property | Value | Test method |
|---|---|---|
| Appearance | Clear | TM 2265 |
| Solids content | 48–54% | TM 2033 |
| Viscosity at 23°C | 130–170 mPa·s | TM 2013 |
| Gel time, table states 66°C to 88°C | 3.5–5.5 minutes | TM 2253 |
| Cure time, table states 66°C to peak | 5–7 minutes | TM 2253 |
| Peak temperature | 220–240°C | TM 2253 |
| Flash point | 33°C | TM 2800 |
The source table lists reactivity intervals starting at 66°C, while the footnote identifies TM 2253 at 82°C using 100 g resin with 2.0 g CH-50. Ask the manufacturer to confirm the applicable test temperature in the latest TDS before using these figures as acceptance criteria. Heated laboratory reactivity values do not establish the pot life or line speed of an actual filled production mixture.
Typical unfilled casting properties
| Property | Value | Test method |
|---|---|---|
| Tensile strength | 65 MPa | ISO 527-2 |
| Tensile modulus | 3.0 GPa | ISO 527-2 |
| Elongation at break | 2.5% | ISO 527-2 |
| Flexural strength | 110 MPa | ISO 178 |
| Flexural modulus | 3.0 GPa | ISO 178 |
| Heat deflection temperature | 105°C | ISO 75 |
| Unnotched impact strength | 10 kJ/m² | ISO 179 |
The Palatal XF 9012 casting data use 1.0 g Butanox M50 and 1.0 g accelerator NL 49P per 100 g resin, followed by 24 hours at room temperature and 24 hours at 80°C. HDT specimens receive a further two hours at 100°C. Testing conditions are 23 ± 2°C and 50 ± 5% relative humidity. These are typical unfilled resin results. Filled, reinforced parts need validation under their own formulation and cure schedule.
Curing and processing guidance
Palatal XF 9012 is supplied without accelerator. For room temperature curing, the PDS calls for a suitable cobalt accelerator system. Pultrusion cure selection depends on equipment, component design, processing temperature and pulling speed. Select and validate the initiation system with technical support. Recommended workshop conditions are 18–32°C and 40–90% relative humidity. Keep conditions consistent and evaluate wetting, cure development and profile quality during production trials.
4 essential checks for better resin selection
1. Define the required fire test. Identify the applicable standard and the finished part construction. The supplied document gives no named fire classification, smoke test result or toxicity certificate. Obtain relevant test reports for the actual formulation and component.
2. Confirm filler and reinforcement. Review aluminium hydroxide loading, particle characteristics and glass content. Palatal XF 9012 supports high filling, but the final formulation must retain suitable flow, impregnation and structural performance.
3. Validate process settings. Establish cure behavior on the actual line with your selected initiator system. Confirm the reactivity test temperature with the manufacturer before comparing incoming batch data against the supplied table.
4. Check supply documentation. Confirm the complete grade, packaging, batch traceability, delivery schedule and remaining shelf life. Request current technical and safety documents when preparing a purchase or production trial.
Storage and Palatal XF 9012 TDS requests
The storage guidance specifies original, undamaged packaging in a dry indoor area at 5–30°C, with prompt use. Avoid direct sunlight, heat sources and open flames. The liquid resin table gives a four-month storage period in the dark at 25°C. Confirm the applicable stability conditions and remaining shelf life with the supplier, and follow the current SDS for safe storage and handling.
For a Palatal XF 9012 supplier enquiry, share your application, process, target fire standard, quantity and destination. Request the latest Palatal XF 9012 TDS, SDS and quotation. This summary uses the Chinese manufacturer PDS, version 1.0 dated 7 August 2020. Browse our AOC resin range and the official AOC product brands for further manufacturer information.